Top 10 Vacuum Hydrocarbon Cleaning Machine Manufacturers
Selecting among Vacuum Hydrocarbon Cleaning Machine Manufacturers takes more than comparing machine sizes or quoted prices. The right system must suit the parts, soil types, throughput, and drying requirements of a real production line. A batch of oily metal components with narrow passages, for example, may need different process settings from flat parts cleaned in large baskets. Details matter.
This guide introduces ten manufacturers and the equipment considerations buyers can use to assess them. Look for clear process descriptions, chamber capacity, vacuum-cycle options, solvent recovery features, and accessible technical support. Ask for documentation that confirms performance claims, plus references from applications similar to yours. A showroom demonstration can help, but it may not represent your actual parts or workload.
Small differences count.
A careful evaluation should also consider operator training, maintenance access, and how the machine fits existing workflows. These points are easy to overlook when a specification sheet looks impressive. There is no single machine that suits every factory, and a top-ten list cannot replace a process trial. Use it as a starting point, then verify the details with each supplier.
Vacuum Hydrocarbon Cleaning: Process Principles and Key Performance Metrics
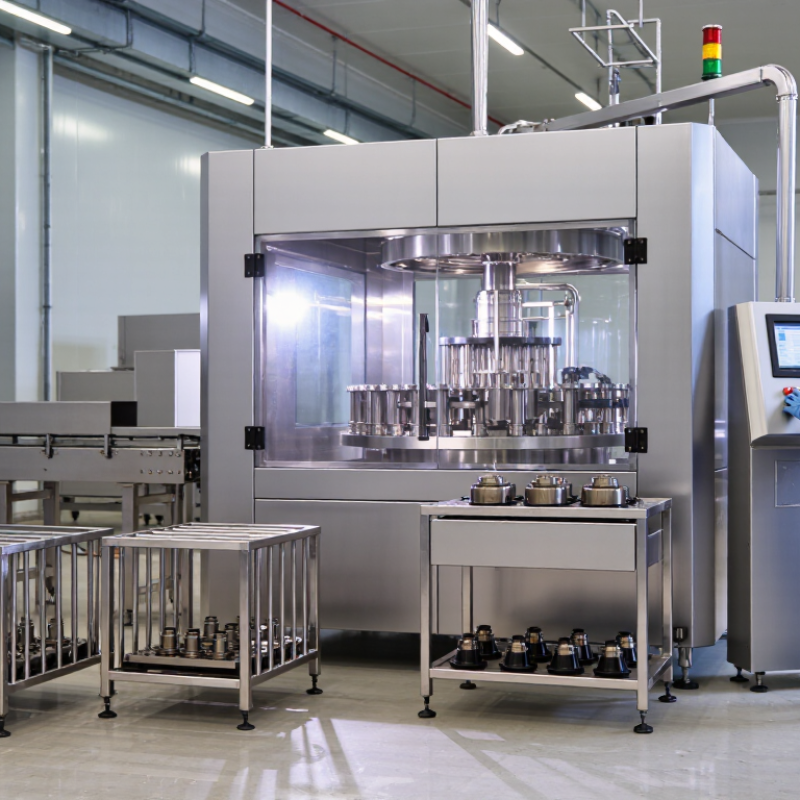
Vacuum hydrocarbon cleaning uses a sealed chamber and a low-residue solvent to remove oils, greases, and similar process soils. Parts are immersed or sprayed, sometimes with ultrasonic energy to loosen contamination from small recesses. The exact sequence depends on the part and soil. Then the solvent is drained. A vacuum stage helps evaporate remaining solvent at a lower temperature, supporting drying without excessive heat.
Performance should be judged with measurable results, not appearance alone. Check residual contamination using a method suited to the part, such as a controlled wipe test or particle analysis. Record drying time, cycle time, solvent consumption, and batch-to-batch consistency. A clean-looking surface can still retain residue in blind holes. That detail matters.
Vacuum level and temperature also affect repeatability. Track chamber pressure, solvent condition, and any signs of leakage; compare readings against the equipment’s validated operating range. Test representative parts with realistic soil loads, including narrow channels and threaded features. One awkward truth: a faster cycle is not always a better one. It may leave wet pockets or uneven cleaning, so verify results before changing settings.
Industry Benchmarks: Chamber Capacity, Cycle Time, and Solvent Recovery
When comparing vacuum hydrocarbon cleaning machines, chamber volume matters only when it matches the parts basket and loading pattern. A practical screening range is 100–300 L for small precision parts and 500–1,000 L for larger batches. These are purchasing benchmarks, not universal industry averages. Leave room around each basket; crowded loads can restrict solvent flow and extend drying.
Cycle time needs a clear test condition. For moderately oily parts, compare quoted cycles around 15–30 minutes; blind holes, dense loads, or heavier residues may require 30–60 minutes. Ask suppliers to run the same representative parts and report cleaning, rinsing, and vacuum-drying times separately. Shorter is not always better. The U.S. EPA’s Control Techniques Guidelines for Industrial Cleaning Solvents discusses process controls, while the European Commission’s surface-treatment BREF identifies solvent recovery and reuse as relevant techniques; neither sets one universal machine cycle or chamber-size benchmark.
For recovery, request a measured solvent mass balance, not a brochure percentage. A 95% recovery target can serve as a screening threshold, provided the test states solvent type, load, and measurement method. Check makeup solvent use over repeated cycles, along with filter changes and distillation losses. Small leaks or wet parts can distort results. Reported figures should be verified under the buyer’s actual operating conditions.
Top 10 Vacuum Hydrocarbon Cleaning Machine Manufacturers - Industry Benchmarks: Chamber Capacity, Cycle Time, and Solvent Recovery
Indicative planning ranges for common industrial machine configurations—not ranked manufacturer specifications or guaranteed performance. Actual results depend on part geometry, soil load, basket loading, solvent, process recipe, and equipment design.
| Benchmark Profile | Typical Usable Chamber Capacity | Indicative Cycle Time | Solvent Recovery Planning Range | Typical Application / Consideration |
| 1. Compact batch unit | 20–50 L | 15–35 min | Approximately 95–99% | Small precision parts and low-volume production; cycle time depends strongly on drying requirements. |
| 2. Small production batch unit | 50–100 L | 20–40 min | Approximately 95–99% | Repeated batch cleaning of machined components; basket loading affects throughput. |
| 3. General-purpose batch unit | 100–200 L | 20–45 min | Approximately 95–99% | Common production scale for mixed component sizes; verify chamber dimensions as well as volume. |
| 4. Large batch unit | 200–400 L | 25–55 min | Approximately 95–99% | Larger parts or higher batch mass; heavy soil loads may require longer filtration and distillation intervals. |
| 5. Extra-large batch unit | 400–800 L | 30–60 min | Approximately 95–99% | High-capacity batch work; confirm usable basket dimensions and plant utility requirements. |
| 6. Multi-stage batch system | 80–300 L per chamber | 20–50 min per load | Approximately 95–99% | Separate wash and rinse stages can support repeatable processes; total throughput depends on stage sequencing. |
| 7. High-throughput batch system | 150–500 L | 15–40 min per load | Approximately 95–99% | Designed around frequent loading and unloading; automated handling can reduce non-cleaning time. |
| 8. Precision-parts configuration | 30–150 L | 20–60 min | Approximately 95–99% | Fine passages and sensitive surfaces may require tailored spray, immersion, or vacuum-drying steps. |
| 9. Heavy-soil configuration | 100–400 L | 30–60+ min | Approximately 95–99% | For oily or particulate-loaded components; filtration capacity and residue management are key selection factors. |
| 10. Automated production-cell configuration | 100–500 L per chamber | 20–50 min per load | Approximately 95–99% | May include conveyors or robotic loading; compare overall line takt time, not just the cleaning cycle. |
Note: Solvent recovery figures are indicative planning ranges, not certified efficiency ratings. Request a documented recovery test and a representative-part cycle trial when comparing equipment.
Cleaning Validation Under VDA 19.1 and ISO 16232
Top 10 Vacuum Hydrocarbon Cleaning Machine Manufacturers
Cleaning Validation Under VDA 19.1 and ISO 16232
A vacuum hydrocarbon cleaning machine can remove oils from complex components, but a clear-looking surface is not proof of cleanliness. Validation should connect the cleaning process to the part’s actual use and contamination risks. VDA 19.1 and ISO 16232 provide methods for assessing particulate cleanliness; they do not certify a machine on their own.
Start with representative parts, including difficult features such as blind holes, narrow channels, and threaded areas. Define sampling locations, extraction methods, and acceptance criteria before testing. Record key process settings, such as wash time, solvent temperature, and drying conditions. Then assess extracted particles using suitable filtration and analysis methods. Keep test conditions consistent. Otherwise, comparisons can mislead. A common weakness is sampling only easy-to-reach surfaces; the resulting data may look reassuring but miss trapped residue. Validation may also need review after process changes.
Tips: Use clean containers and gloves when handling tested parts. Label samples immediately. Keep extraction blanks in the plan, and document any deviations. Small details matter. Revisit criteria when part geometry or customer requirements change.
Top 10 Vacuum Hydrocarbon Cleaning Machine Manufacturers Compared
Top 10 Vacuum Hydrocarbon Cleaning Machine Manufacturers Compared
A useful comparison looks beyond advertised tank volume. Check vacuum range, heating control, basket dimensions, and the filtration stages included as standard. These details affect how reliably a machine cleans small metal parts with blind holes or narrow channels. Ask for cycle data using parts similar to yours.
Compare throughput under realistic conditions, not just the shortest cycle shown in a brochure. A larger chamber may fit more baskets, but heating and drying can take longer. Review solvent recovery design, maintenance access, operator training, and the availability of process documentation. Request written performance figures and clarify which options change the price. That matters. Comparisons can still be imperfect: test parts, loading patterns, and soil levels vary between facilities.
Tips: Ask each manufacturer for a sample cycle plan, utility requirements, and a maintenance schedule. Check whether filters and seals are easy to inspect. Look closely. A short demonstration with your own parts can reveal residue or drying issues that specifications may miss.
Solvent Safety: NFPA 30 Flash-Point Thresholds at 37.8°C and 60°C
NFPA 30 classifies liquids with flash points from 37.8°C to below 60°C as Class II, and from 60°C to below 93°C as Class IIIA. These are classification thresholds, not temperatures at which a solvent becomes harmless. A vacuum hydrocarbon cleaning machine can reduce solvent exposure through a sealed process, but vapors may still escape during charging, draining, or maintenance. A few degrees matter. Check each solvent’s safety data sheet and confirm the machine’s design suits its flash point and operating conditions.
Tips: Ask manufacturers how they manage vapor recovery, grounding, leak detection, and safe access for maintenance. Verify that temperature controls and alarms match the solvent’s documented properties. NFPA 30 and OSHA 29 CFR 1910.106 provide established guidance on liquid classifications and handling; use the applicable requirements for your site. Keep SDS documents near the cleaning area, not buried in a purchasing folder.
When comparing equipment suppliers, request test records for the intended solvent, not just general performance figures. Check seals, hoses, and recovery connections for compatibility. Confirm who inspects the system and how often. Flash point alone does not describe every hazard; it does not measure toxicity or guarantee safe operation under vacuum. That distinction is easy to overlook, even in a well-equipped workshop. A careful review should include process temperature, ventilation, ignition-source control, and operator training.
Solvent Safety: NFPA 30 Flash-Point Thresholds
Key flash-point boundaries used to classify flammable and combustible liquids (°C).
Under NFPA 30, Class I liquids have flash points below 37.8°C; Class II liquids range from 37.8°C to below 60°C; Class IIIA liquids range from 60°C to below 93.3°C; and Class IIIB liquids have flash points of 93.3°C or higher. Confirm the applicable requirements against the current code edition, the solvent’s safety data sheet, and local regulations.